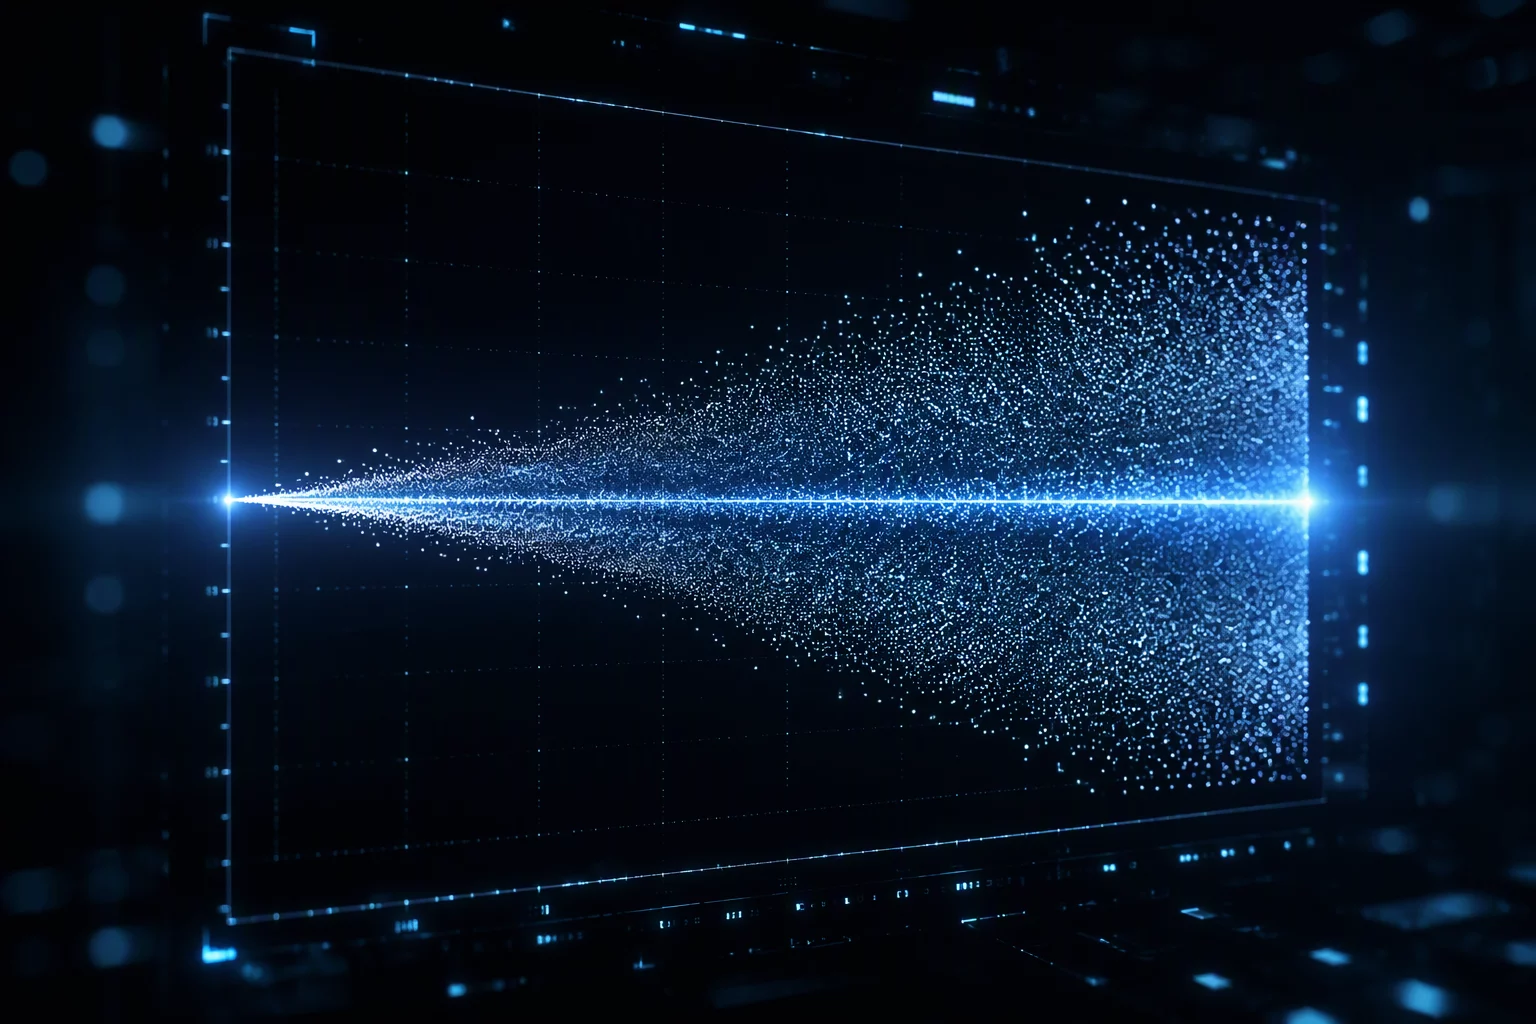
The Masking Effect of Symmetrical Process Spread
Monitoring solely through location parameters creates an illusion of process control, as expanding variation frequently balances symmetrically around the nominal target.
When production units leave an assembly station, quality teams routinely report the subgroup mean to track alignment. Over forty-two monitored production cycles, the grand average remained tightly centered at 24.02 millimeters with zero statistical shift. Unbeknownst to plant supervisors, the individual readings were fanning outward toward the upper and lower specification limits. Because the deviations occurred symmetrically, positive errors canceled out negative errors in every calculated average.
- Overall process centering maintained near-perfect alignment at 24.02 mm.
- Subgroup standard deviation expanded by 142% over 42 cycles.
- Classical run charts on sample averages showed zero alarm signals.
The operational danger lies in false assurance. An engineering team evaluating only the X-bar chart assumes the tooling is operating under stable conditions. Meanwhile, internal mechanical play in clamping fixtures gradually expands cycle-to-cycle variation until components begin failing downstream fit checks.
“Central tendency describes the position of the process, but dispersion reveals its health. Never interpret a stable mean without first verifying the stability of variation.”
Dissecting Subgroup Sigma and Range Metrics
To uncover the underlying instability, the data was re-evaluated through paired X-bar and S control charts. While the X-bar control chart showed all subgroup averages safely within control limits, the S chart exhibited seven consecutive points above the central line followed by multiple points exceeding the upper control limit. This pattern confirms that the variation itself was not in statistical control.
Further decomposition showed that while within-subgroup variation was swelling, between-subgroup averages remained stationary. The culprit was identified as uneven thermal expansion in the guide rails during extended shifts. The thermal gradient introduced loose tolerances without skewing the process systematically in one direction. Consequently, the capability metric Cpk deteriorated from 1.62 to 0.81, even though the process never experienced a mean shift.
Detection Strategies and SPC Best Practices
Rigorous statistical quality control mandates that the dispersion chart—whether an R chart or an S chart—must be evaluated and proven stable before any interpretation of the mean chart is valid. If the dispersion chart is out of control, the control limits on the mean chart are invalid because they rely on an unstable estimate of within-subgroup variation.
Manufacturing engineers should set up real-time alarms on moving range and subgroup standard deviation rather than relying solely on grand averages or end-of-line pass rates. Conducting periodic variance-ratio tests and inspecting individual value distributions prevents hidden variation from compromising product conformance.
Related Articles
Frequently Asked Questions
A sample average is a measure of central tendency calculated by summing values and dividing by sample size. When a process experiences expanding variation that is symmetrical, high and low deviations cancel each other out, leaving the average unchanged despite wider dispersion.
The dispersion chart (S chart or R chart) must always be examined before the mean chart (X-bar chart). If dispersion is out of statistical control, the control limits on the mean chart are mathematically invalid.
Capability metrics inversely correlate with process spread (6 sigma). When variation increases, the denominator in capability formulas expands, causing both Cp and Cpk to drop sharply even if the process remains centered on target.
Key Analytical Takeaways
Statistical control limits for the mean depend on a stable estimate of sigma; unverified dispersion renders mean interpretations invalid.
Symmetrical variations neutralize each other within calculated averages, producing an illusion of process stability.
Expanding standard deviation degrades capability indices like Cpk well before the central tendency registers any measurable shift.
Request Analytical Consultation
Inquire directly on statistical baseline validation and review specific parameters of this case.