Navigating Conflicting Targets in Multivariate Systems
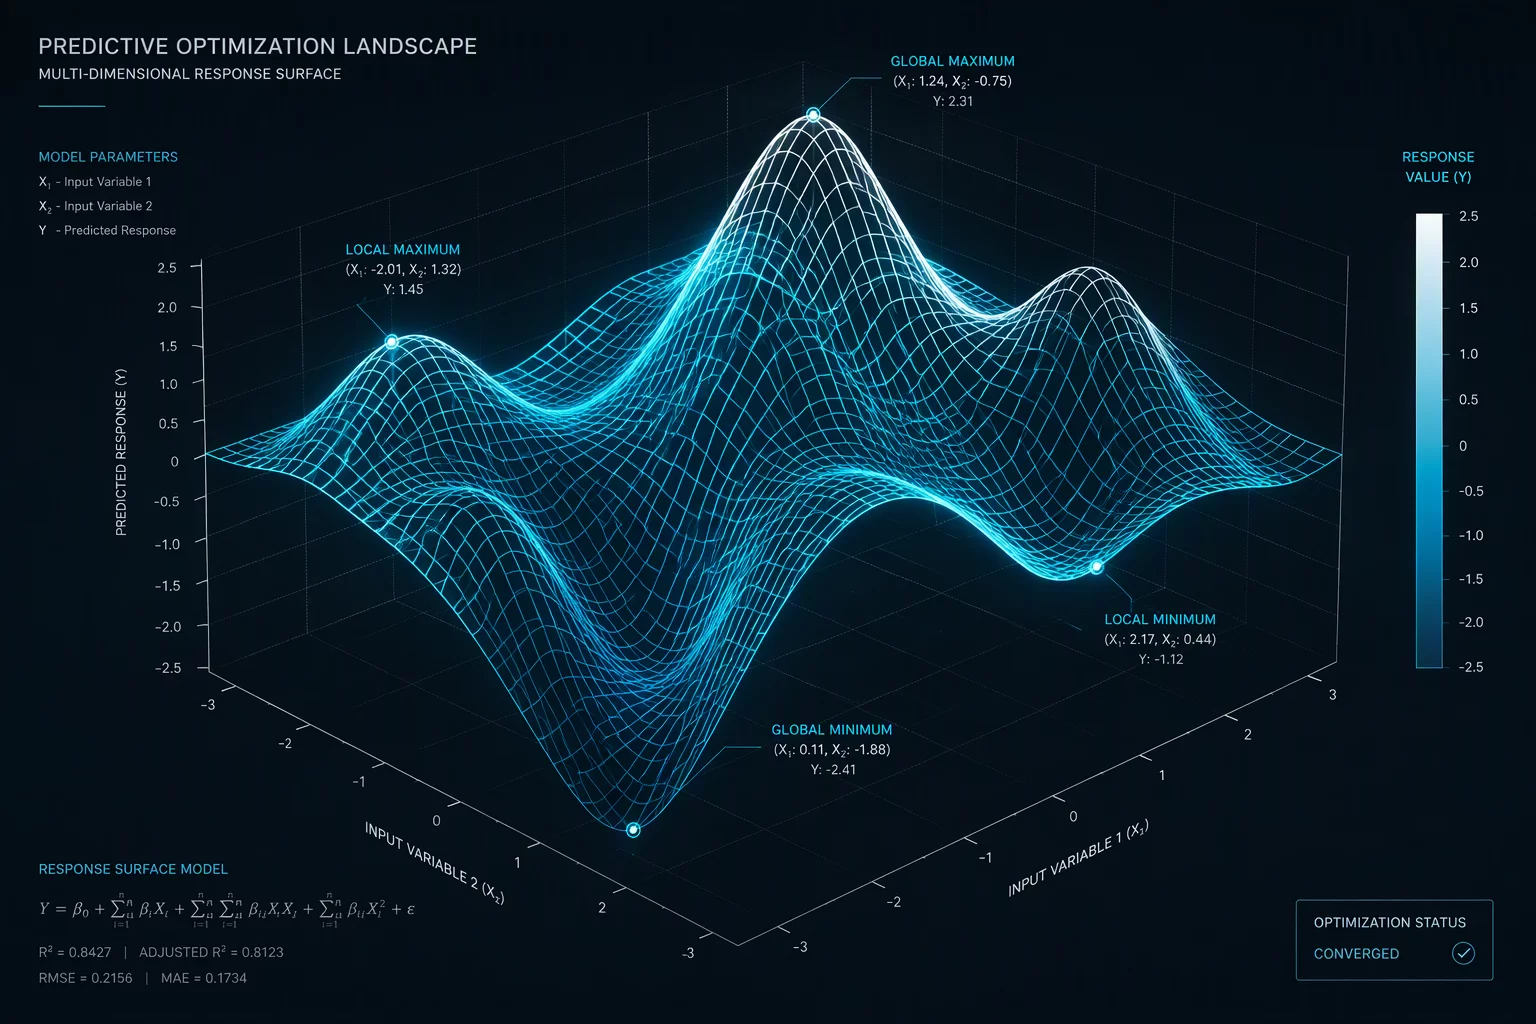
Manufacturing processes rarely hinge on a single quality metric. Operating teams regularly balance tensile strength against elongation, or dimensional accuracy against production cycle time. Multiple response optimization resolves this tension by mapping mathematical relationships across separate output channels simultaneously. Rather than isolating each variable in independent regression formulas, empirical modeling constructs a continuous response surface where every factor adjustment evaluates its joint consequence across all target outputs.
Predictive modeling establishes the underlying mathematical boundaries across operating conditions. Engineers calculate quadratic response surfaces to detect curvature, ridge lines, and saddle points within the experimental space. When target responses compete directly against one another, single-objective algorithms fail by pushing one attribute into defect zones. Multi-response frameworks assign individual desirability curves to each output, merging them into an overall composite desirability index that guides automated or operator-driven setpoint decisions.
Consultation Protocol
Request an Analytical Model Review
Submit production parameters and active factor matrices to calibrate multi-response prediction intervals with our engineering team.
Core Summary
Key Principles for Stable Optimization
Composite desirability functions prevent local sub-optimizations by forcing all critical response variables into simultaneous compliance windows.
Polynomial model adequacy requires rigorous verification of residual normality, constant variance, and lack-of-fit testing prior to sweet spot searches.
Extrapolation outside verified factor ranges introduces severe prediction distortion; operating setpoints must remain inside experimental boundaries.
An optimum that satisfies three variables while destabilizing a fourth is merely a planned failure. True predictive modeling defines operating windows where every parameter remains safely within control limits.
Advanced Systems Analysis Group
System Execution
Technical Execution Protocol for Multi-Response Modeling
Implementing predictive models begins with structured design matrices and noise factor isolation. The modeling engine fits individual second-order equations for each designated response variable, isolating main effects, two-way interaction terms, and quadratic curvature. Technicians examine coefficient significance through analysis of variance (ANOVA) tables, eliminating non-significant terms to avoid overfitting while preserving model hierarchy.
Once baseline equations demonstrate adequate predictive power, individual desirability functions scale each response onto a dimensionless scale between zero and one. A value of zero represents unacceptable behavior, while one represents target perfection. The geometric mean of these individual functions yields the overall composite desirability score, transforming a complex multi-criteria challenge into a single solvable optimization surface.
Stepwise Multi-Objective Optimization Procedure
Design Matrix Screening: Execute full factorial or response surface design runs to capture factor interactions and system non-linearities across production windows.
Individual Response Fitting: Calculate regression coefficients, verify lack-of-fit metrics, and inspect standardized residuals across each dependent variable independently.
Desirability Profile Calibration: Assign target bounds, acceptable limits, and shape exponents for each response to mirror operational priorities and engineering constraints.
Numerical Surface Maximization: Run gradient search algorithms across the continuous factor domain to locate robust coordinate setpoints maximizing joint composite desirability.
Analytical Evaluation
Validation Limits and Model Boundary Verification
Confirmation runs are vital before deploying newly calculated setpoints onto production machinery. Field validation requires producing small verification batches at the optimal factor settings, measuring all responses, and checking whether empirical observations fall within calculated 95% prediction intervals. Discrepancies often signal unaccounted environmental noise or subtle drift in raw feedstocks.
Periodic model recalibration guarantees ongoing predictive fidelity. When equipment components undergo maintenance or ambient operating temperatures undergo seasonal shifts, predictive surfaces must incorporate refreshed baseline samples. Keeping active logs of process inputs alongside predictive variance outputs maintains high fidelity in process stability.
Related Material
Complementary Predictive and Analytical Guides
Analytics
AI Driven Analytics for Process Windows
Algorithmic boundary detection and automated parameter threshold classification for modern manufacturing lines.